Business Details
Durable Industrial Flooring Solutions in Grand Falls
Tufco Flooring has been a trusted name in industrial and commercial flooring solutions for over 35 years. Our team of specialists is dedicated to delivering high-durability, sanitary flooring systems tailored to withstand the toughest environments, including food processing plants, dairies, and pharmaceutical facilities. We prioritize meticulous surface preparation to ensure long-lasting finishes that meet or exceed CFIA, USDA, and FDA standards. Our commitment to quality extends to using advanced materials like urethane and epoxy, which offer resistance to thermal shock, chemicals, and heavy machinery.With flexible scheduling, including weekend operations, we minimize downtime for clients while maintaining strict adherence to project timelines. Our 5-year warranty reflects confidence in the reliability of our products and services. Serving the Maritimes and Quebec, we combine technical expertise with personalized support to address each client's unique needs. From drainage solutions to decorative flooring, our comprehensive approach ensures functional and aesthetic excellence. This legacy of experience positions us as a leader in industrial flooring innovation.
Services
Industrial Flooring
Urethane Flooring
Epoxy Flooring
Drainage Systems
Decorative Flooring
Highlights and features
- We offer 35+ years of specialized industrial flooring expertise.
- Our team provides flexible scheduling to minimize operational downtime.
- We use materials meeting CFIA, USDA, and FDA compliance standards.
- We guarantee a hassle-free 5-year warranty on all installations.
- Our seamless flooring systems resist chemicals, thermal shock, and heavy machinery.
Associations and certifications
- CFIA
- USDA
- FDA
Services
Industrial Flooring
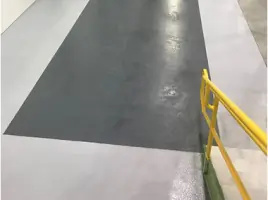
Tufco Flooring's industrial flooring systems are engineered for extreme environments. Our solutions combine urethane and epoxy materials to create seamless, chemical-resistant surfaces that withstand thermal shock, heavy machinery, and high-traffic areas. Ideal for food processing plants, pharmaceutical facilities, and cold storage units, these floors meet CFIA, USDA, and FDA standards. The 3/8" Tufcrete hybrid topping provides maintenance-free durability while allowing rapid return to service after installation.
Urethane Flooring
Our urethane flooring solutions offer unmatched resistance to thermal cycling and mechanical stress. Designed for environments requiring steam cleaning and exposure to caustic chemicals, these seamless systems prevent bacterial growth in food processing areas. The formulation maintains structural integrity under extreme temperature fluctuations and heavy forklift traffic. Applications include beverage plants, meat packing facilities, and pharmaceutical manufacturing where hygiene and durability are critical.
Epoxy Flooring
Tufco Flooring's epoxy flooring provides a non-porous, odorless surface with exceptional tensile strength. The multi-layer application creates a resin-rich finish that resists abrasion and chemical exposure while maintaining slip resistance. Ideal for CIP areas and commercial kitchens, this system eliminates annual reapplication through its permanent bond and moisture-proofing properties. The quick-cure formula minimizes downtime during installation.
Drainage Systems
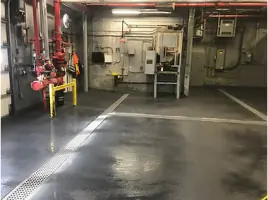
Custom stainless steel drainage solutions handle high-volume wastewater in industrial settings. The TD Series box drains and trench systems feature heavy-duty gratings and welded construction to prevent leaks. Available with multiple customization options, these systems integrate seamlessly with flooring installations. The exposed discharge pipe design simplifies maintenance while meeting strict sanitation requirements for food processing environments.
Decorative Flooring
Functional yet visually appealing flooring options enhance commercial spaces. Available in flake and quartz formulations, these systems provide slip-resistant surfaces for offices, washrooms, and lunchrooms. The decorative finishes maintain industrial-grade durability while offering customization through color and texture variations. Seamless application ensures easy cleaning and long-term performance in moderate-traffic areas.
Questions
What industries do your flooring systems serve?
Our flooring solutions cater to food processing plants, dairies, pharmaceutical facilities, beverage production, cold storage units, and commercial kitchens requiring durable, sanitary surfaces.
Do you offer warranties on your installations?
Yes, we provide a hassle-free 5-year warranty covering material defects and workmanship for all our flooring systems.
Can you install flooring in large facilities?
We handle projects ranging from 1,000 sq. ft. to 225,000 sq. ft., with flexible scheduling to minimize operational disruption during installation.
What regions do you service?
We serve commercial clients across the Maritime provinces and Quebec, with specialized installation teams available for large-scale projects.
How do your floors handle extreme temperatures?
Our urethane systems withstand thermal shock from -40°C to 120°C, making them ideal for freezers, fryer lines, and steam-cleaned environments.
Can you repair existing flooring?
Yes, we assess existing floors for repairability and offer slope correction services to eliminate water pooling while maintaining seamless integration with new installations.